 |
| September 22, 2026 | Volume 22 Issue 36 |
Designfax weekly eMagazine
Archives
Partners
Manufacturing Center
Product Spotlight
Modern Applications News
Metalworking Ideas For
Today's Job Shops
Tooling and Production
Strategies for large
metalworking plants
How to master metal powder management in 3D printing
By Tim Wischeropp, CEO and Co-Founder, amsight
Powder-bed fusion has a strange contradiction built into it. We invest in precision machines, tightly controlled atmospheres, meticulous parameter sets, and expensive inspection. We talk about "industrialization" and "serial production." Then we manage one of the most critical variables in the entire process chain (the powder) like it's a static material that arrived with a certificate.
That approach was understandable in the early days or prototyping. It is not sustainable in production for critical parts. Why? Because powder is not static. Powder is history.
Every cycle, every handling step, every exposure, and every mixing decision changes it, sometimes subtly, sometimes measurably, and sometimes in ways that only show up downstream as scatter, drift, and scrap. And if you want AM to behave like a mature manufacturing technology, you must treat powder management not as housekeeping, but as process control.
The real cost of "good enough" powder tracking
Most teams don't have a powder problem until they do. At low scale, spreadsheets feel fine. You can track batch numbers, write down re-use counts, and rely on experience, but as soon as you add machines, materials, customers, and auditors, the cracks appear in predictable ways:
- Blend ratios get lost across files.
- Powder states become ambiguous ("sieved, but when?" "unsieved, from which cycle?").
- Quality results are stored without powder context.
- When a failure happens, the first hours are spent reconstructing history instead of solving the engineering problem.
This is the hidden cost. Not only the scrap itself, but the wasted senior time spent doing "powder archaeology."
What changes in powder isn't theoretical
We know from both literature and shop-floor experience that powder changes across re-use in multiple dimensions: chemistry shifts (oxygen/hydrogen uptake) and morphology changes to affect flow, PSD drift, and contamination (see Figure 1 and Figure 2). These changes are gradual, which is exactly why they cause so much damage. Gradual drift doesn't trigger alarms. It simply widens variation until you cross a limit.
When you cross a limit, the factory reacts the only way it knows how: inspect more, CT more, test more, refresh more. That's not optimization. That's fear.
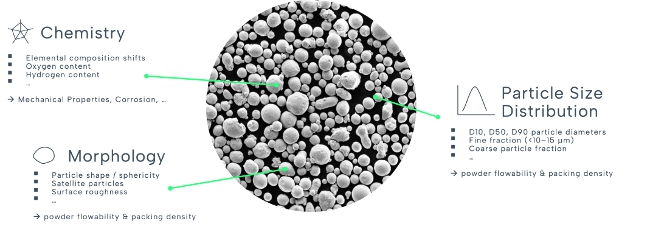
Figure 1: Typical powder properties that change over re-use for metal AM.
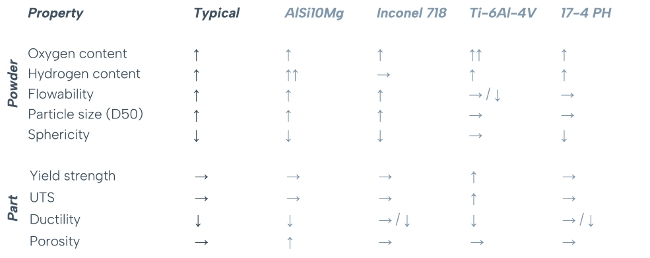
Figure 2: Typical influence of powder re-use over time in metal AM. [Credit: Image courtesy of amsight]
There is no universal "best" re-use strategy
One of the most common questions we get at amsight is, "Which re-use strategy is the right one?" The honest answer is, it depends on your priorities (see Figure 3 and Figure 4).
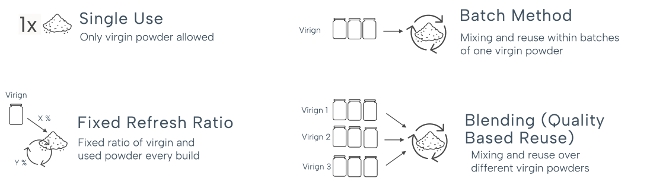
Figure 3: Overview on dominant powder re-use strategies in powder-bed AM. [Credit: Image courtesy of amsight]
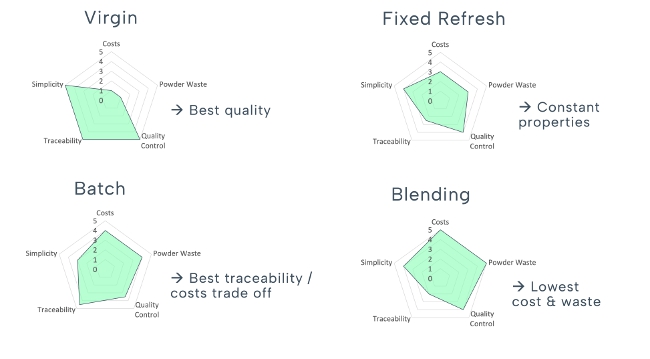
Figure 4: Comparison of powder re-use strategies in terms of costs, powder waste, quality control, traceability, and simplicity (0 = very bad; 5 = very good). [Credit: Image courtesy of amsight]
There is no one-size-fits-all strategy. The optimal strategy is the one that meets your quality and regulatory requirements, is manageable on the shop floor, and is supported by evidence, not hope. And this last point matters. In regulated industries, even blending can be acceptable, but acceptance is earned. It must be discussed with the customer. It must be supported by data. Trust is not a feeling; it is documentation plus stability evidence.
From certificates to cycles
To master powder management, we need to change how we think about the powder record. A certificate tells you what the powder was when it arrived. Production needs to know what the powder became. That is why we talk about a digital powder history, a part-linked record that captures each cycle, each mixing event, and the powder state behind each build (see Figure 5 and Figure 6). When you have that history, the conversation changes.
Instead of asking, "Which batch was this?" you can ask:
- How old was this powder in terms of re-use and exposure?
- Which virgin lots contributed to this blend, and in what ratios?
- Which builds consumed it, and what were the outcomes?
- What did we observe in CT, mechanical tests, and surface quality, and how did that trend over time?
This is where powder management becomes a competitive advantage. You can detect drift early, reduce refresh conservatism, and lower scrap without gambling on intuition.
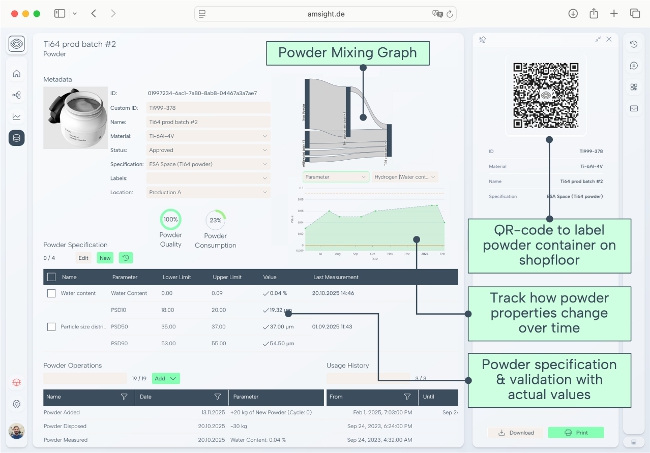
Figure 5: Full powder history in amsight -- from mixing and usage history to change-of-powder properties of time. This level of powder tracking is essential to be able to understand the effect of powder handling on powder properties and to optimize powder usage strategy based on data. [Credit: Image courtesy of amsight]
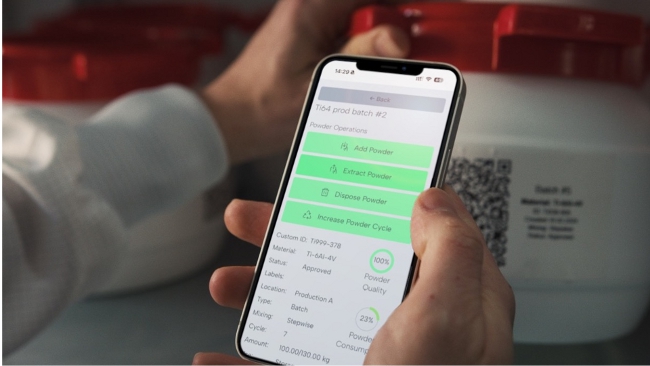
Figure 6: Track and document powder handling on the shop floor with QR codes and amsight's dedicated shop-floor app. [Credit: Image courtesy of amsight]
Data-driven powder management
In a recent webinar Q&A, we made a point that surprised some people: The "most important powder parameters" depend on material and strategy, and transferability between organizations is limited. Some hear that and feel discouraged. They shouldn't.
It's good news, because it means you can build a competitive edge. If you identify your own CTQs (Critical to Quality metrics), correlate them to part outcomes in your environment, and then apply SPC (Statistical Process Control) to trend stability, you're no longer guessing. You're running powder management as a controlled process.
That's the essence of industrial maturity: fewer heroic decisions, more repeatable rules backed by evidence.
SPC in powder management
If there is one discipline that AM production must embrace more seriously, it is Statistical Process Control. SPC turns "I think it's okay" into "I can show it is stable." It allows you to (see Figure 7):
- Detect drift before parts go out of spec.
- Quantify process capability.
- Reduce the need for over-inspection.
- Optimize refresh rates and characterization effort based on evidence.
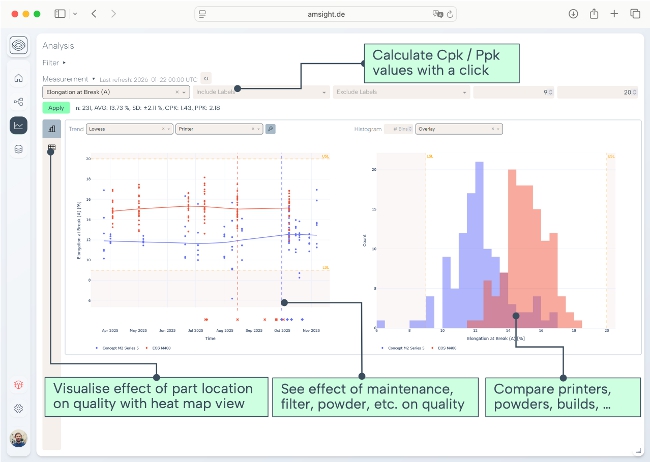
Figure 7: Monitor quality over time and understand how powder re-use affects the overall part quality. [Credit: Image courtesy of amsight]
amsight for powder lifecycle management
We built amsight because we kept seeing the same bottleneck. Teams weren't short of data; they were short of connected data.
Powder management is a perfect example. When tracking lives in spreadsheets, the story is fragile. That's why the powder management approach on our platform focuses on QR-based tracking and full genealogy -- capture each step, record each blend, link powder to builds and outcomes, and make the history queryable, not just stored (see Figure 6).
The intent is simple: Stop relying on memory and estimates. Make powder condition measurable and actionable.
A pragmatic starting point
If you want to improve powder management without turning it into a multi-year transformation, start with three questions:
- Do you have a real-time overview of inventory and powder state (sieved/unsieved, location, quantity)?
- For a part printed two months ago, can you retrieve powder history and inspection outcomes within minutes?
- Do you know your CTQs, and do you trend them over time?
This is how AM becomes more reliable and more cost efficient, not by adding complexity, but by controlling the variables that matter.
Learn practical powder management and SPC for AM
We're continuing this discussion in our on-demand webinars on "Mastering Powder Management in AM" and "Statistical Process Control in AM: From Data to Process Stability and Repeatable Part Quality" with registration available here:
amsight.de/webinars/mastering-powder-management-in-am
amsight.de/webinars/statistical-process-control-in-am
Because in production AM, quality is not what you measure once. It is what you can keep stable, build after build, month after month.
Learn more and see all of amsight's capabilities at amsight.de.
Published September 2026
Rate this article
View our terms of use and privacy policy